

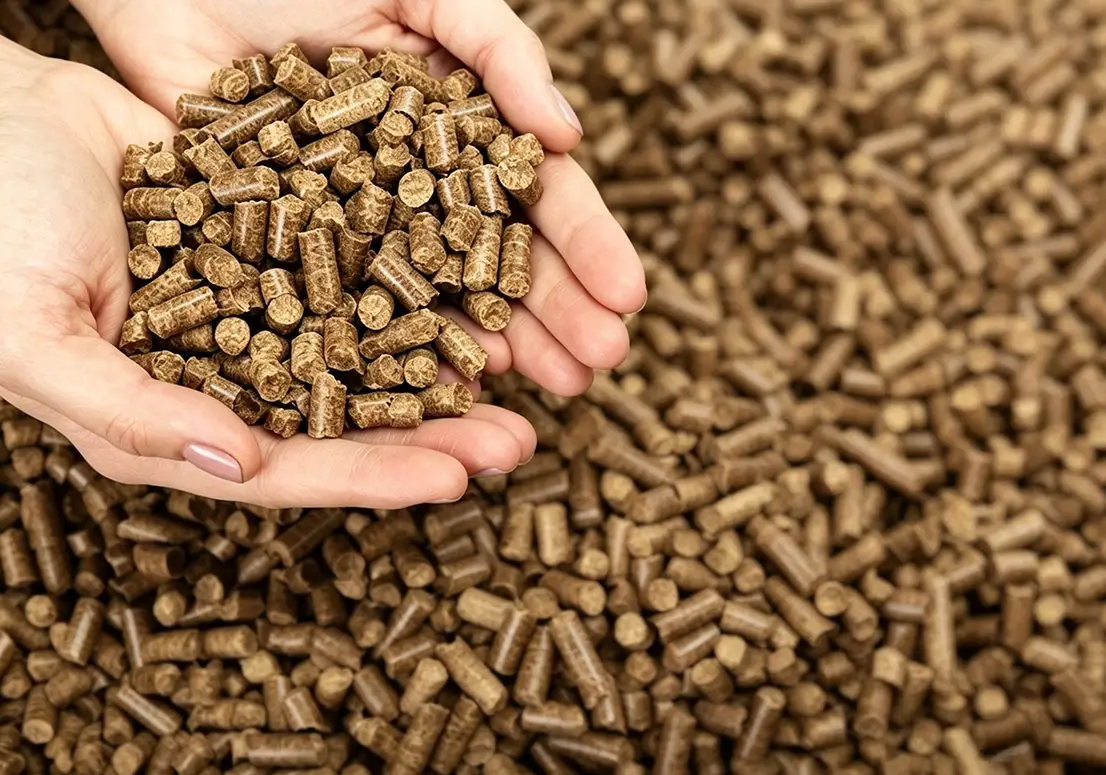
Moisture is one of the most important factors affecting the performance of an EFB pelletizing line. Empty fruit bunches, commonly known as EFB, are a major biomass residue generated during palm oil processing. Unlike some relatively dry biomass materials, freshly collected EFB can contain a considerable amount of moisture. This characteristic directly influences shredding, drying, grinding, feeding, pellet formation, cooling, storage, and final pellet quality.
If the moisture content of EFB is too high, the pellet mill may experience unstable feeding, higher energy consumption, die blockage, low pellet durability, and inconsistent production. On the other hand, if the material is excessively dry, pellet formation can also become difficult because the particles may not bind together effectively under compression.
For this reason, moisture control should be treated as a key part of EFB pellet production rather than simply a drying step before pelletizing.
A well-designed EFB pelletizing process balances moisture with particle size, fiber structure, die compression, feeding rate, and pellet mill operating conditions. This article explains how moisture affects EFB pelletizing results, what happens when EFB is too wet or too dry, how to control moisture, and how moisture management can improve the performance of an EFB pellets machine.
What Is EFB?
EFB stands for empty fruit bunches. It is the fibrous residue remaining after palm fruits are separated from fresh fruit bunches during palm oil processing.
Palm oil mills can generate large quantities of EFB continuously. The material is renewable and can potentially be used as a biomass fuel, but raw EFB has several characteristics that make direct utilization difficult.
These characteristics include:
- High moisture content
- Long and flexible fibers
- Irregular particle size
- Low bulk density
- Difficult material flow
- Variable physical properties
- Potential contamination with soil and other materials
Because of these characteristics, EFB usually requires pretreatment before it can be efficiently pelletized.
Moisture is one of the first properties that should be evaluated when designing an EFB pellet production line.
Why Moisture Matters in EFB Pelletizing
Pelletizing is a compression process.
Prepared EFB enters the pellet mill, where rollers compress the biomass through holes in a die. The particles are forced together under pressure and form cylindrical pellets.
Moisture influences how the particles respond to this compression.
An appropriate amount of moisture can help biomass particles move and bind under pressure. However, excessive moisture can prevent stable pellet formation, while insufficient moisture can make the material too dry and difficult to compact.
Moisture therefore affects:
- Pellet density
- Pellet durability
- Pellet appearance
- Pellet mill capacity
- Energy consumption
- Die performance
- Roller performance
- Feeding stability
- Cooling requirements
- Storage stability
The objective is not simply to remove as much moisture as possible. The goal is to achieve a suitable moisture condition for stable pellet production.
What Happens When EFB Moisture Is Too High?
High moisture is one of the most common problems in EFB pelletizing.
Fresh EFB can be significantly wetter than the material required for efficient pellet production. If wet EFB is sent directly into the pellet mill, several problems can occur.
Poor Pellet Formation
Excessive moisture can make the material too soft and sticky.
Instead of forming firm pellets, the biomass may pass through the die in an unstable manner. Pellets may become soft, deformed, or difficult to cut cleanly.
Lower Pellet Durability
Wet pellets may initially appear to have good cohesion, but excessive moisture can reduce their structural stability.
After cooling and drying, the pellets may shrink, crack, or break.
Higher Energy Consumption
A pellet mill must work harder when the material is not properly conditioned.
At the same time, excessive moisture means that more thermal energy may be required during the drying stage.
This can increase the overall energy cost of the production line.
Die Blockage
Wet and sticky biomass may accumulate inside the die holes.
If the material cannot move through the die smoothly, pressure can increase and production can become unstable.
In severe cases, operators may need to stop the machine and clean the die.
Feeding Problems
High-moisture EFB can have poor flowability.
Fibers may stick together and form bridges inside the hopper. This can cause irregular feeding into the pellet mill.
What Happens When EFB Is Too Dry?
Although high moisture is a common concern, excessively dry EFB can also create problems.
When the material becomes too dry, the particles may have insufficient natural moisture to support stable compression.
Possible effects include:
- Weak pellet formation
- Increased fines
- Poor pellet durability
- More dust
- Higher electrical consumption
- Unstable production
- Excessive die wear in some operating conditions
Very dry biomass can behave more like a loose powder or dry fiber mass.
The material may pass through the compression zone without achieving the desired level of cohesion.
Therefore, over-drying should be avoided.
Finding the Right Moisture Range
There is no universal moisture value that applies to every EFB pelletizing project.
The appropriate moisture condition depends on several factors, including:
- EFB variety and source
- Initial moisture
- Fiber structure
- Particle size
- Pellet diameter
- Die compression ratio
- Pellet mill design
- Production capacity
- Final pellet application
- Ambient conditions
In many biomass pelletizing applications, moisture is controlled within a moderate range before entering the pellet mill. However, the exact target should be established through raw material testing and production trials rather than assuming one fixed value is suitable for every plant.
For commercial EFB projects, laboratory analysis and pilot testing can help determine the optimal operating range.
Moisture and EFB Particle Size
Moisture does not work independently.
Particle size and moisture interact throughout the pelletizing process.
If EFB is too wet and contains long fibers, the material may become difficult to grind and feed.
After drying, the material becomes easier to process through a hammer mill or other grinding equipment.
A relatively uniform particle size can then improve the consistency of compression inside the pellet mill.
This means that moisture control should be coordinated with:
Shredding → Drying → Grinding → Feeding → Pelletizing
Poor performance in one stage can affect the next stage.
How Moisture Affects EFB Grinding
Drying changes the physical characteristics of EFB.
Wet EFB is often more flexible and difficult to reduce into uniform particles. Fibers can bend rather than break, and wet material may stick to equipment surfaces.
After appropriate drying, the material generally becomes easier to crush and grind.
This can improve:
- Hammer mill efficiency
- Screen performance
- Particle size consistency
- Material flow
- Pellet mill feeding
However, excessive drying can increase dust generation during grinding.
Therefore, the drying and grinding systems should be designed as an integrated process.
How Moisture Affects Material Feeding
Stable feeding is essential for pellet mill operation.
An EFB pellet mill requires a continuous and reasonably uniform supply of prepared biomass.
If EFB is too wet, fibers may stick together and create bridging in the hopper.
If EFB is too dry, excessive dust may make feeding more difficult and increase the amount of fine material in the system.
A variable-speed feeder can help regulate material flow.
For industrial plants, the feeding system may include:
- Storage hopper
- Agitator
- Screw feeder
- Variable-frequency drive
- Level sensor
- Automatic control
Maintaining stable feeding helps keep pellet mill load more consistent.
How Moisture Affects Pellet Density
Pellet density is another important result affected by moisture.
During compression, moisture can influence how biomass particles move and fill the spaces between larger particles.
If moisture is within a suitable range, the material can be compressed more effectively.
If the material is excessively wet, the pellet may not achieve the desired structure after leaving the die.
If it is too dry, particle bonding may become insufficient.
The final density depends not only on moisture but also on:
- Particle size
- Raw material composition
- Fiber structure
- Die design
- Compression ratio
- Roller pressure
- Production speed
Therefore, moisture should be adjusted together with the mechanical parameters of the pellet mill.
Moisture and Pellet Durability
Pellet durability describes how well pellets resist breaking during handling, transportation, and storage.
Low durability can lead to:
- More fines
- Higher material loss
- Dust generation
- Poor packaging appearance
- Handling difficulties
Moisture has a direct influence on durability because it affects particle bonding during compression.
However, moisture alone does not determine durability.
A pellet can still have poor durability if:
- Particle size is unsuitable
- The die compression ratio is incorrect
- Rollers are improperly adjusted
- The material is not sufficiently prepared
- Cooling is inadequate
- The pellet mill operates outside its optimal range
Therefore, moisture control should be part of a broader pellet quality management strategy.
How Moisture Affects the EFB Pelletizing Die
The die is one of the most important components of a pellet mill.
When moisture is too high, wet biomass can increase friction and create deposits inside die holes.
This may result in:
- Reduced production
- Increased pressure
- Unstable pellet formation
- Die blockage
- More frequent cleaning
If the material is too dry, excessive friction may also occur depending on the material and operating conditions.
This is one reason why die selection and moisture management must be considered together.
The compression ratio of the die should match the properties of the EFB being processed.
Moisture and Roller Performance
The rollers compress EFB against the die.
Proper roller condition and clearance are important for stable pellet production.
When material moisture changes significantly, the compression behavior of the biomass can also change.
This means that a setting that works well for one moisture condition may not provide the same results when the material becomes much wetter or drier.
Operators should therefore monitor:
- Roller condition
- Roller clearance
- Pellet mill load
- Production rate
- Die pressure
- Pellet appearance
Maintaining consistent raw material conditions can make pellet mill operation more stable.
How Drying Equipment Controls EFB Moisture
The industrial rotary dryer machine is one of the most important machines in an EFB pelletizing line.
For industrial production, a rotary drum dryer is commonly used to reduce moisture from freshly processed EFB.
A typical drying system can include:
- Feeding conveyor
- Rotary drum
- Hot air furnace
- Fan
- Cyclone
- Dust collector
- Exhaust system
- Temperature monitoring system
The dryer should be sized according to:
- Raw EFB capacity
- Initial moisture
- Target moisture
- Available heat source
- Required production rate
An undersized dryer can limit the capacity of the entire pellet plant.
An oversized dryer may increase capital and operating costs unnecessarily.
Why Drying Temperature Alone Is Not Enough
It is a mistake to control EFB drying only by temperature.
Drying performance depends on several factors:
- Hot air temperature
- Airflow
- Residence time
- EFB particle size
- Initial moisture
- Material feeding rate
- Dryer design
- Ambient conditions
Two batches exposed to the same temperature may leave the dryer with different moisture contents if their initial moisture levels or particle sizes are different.
For this reason, moisture measurement at the dryer outlet is important.
Measuring EFB Moisture
Reliable moisture measurement helps operators make better production decisions.
Moisture can be checked using laboratory methods or suitable industrial moisture meters.
Measurements can be taken at several points:
Before Drying
This provides information about the initial condition of the EFB.
After Drying
This indicates whether the dryer is achieving the target condition.
Before Pelletizing
This is especially important because the pellet mill receives the prepared material.
Finished Pellets
Finished-product moisture can help evaluate cooling, storage, and overall process performance.
Regular measurement is more reliable than estimating moisture by appearance or touch.
How to Prevent EFB From Reabsorbing Moisture
EFB can absorb moisture from the surrounding environment.
This can happen after drying but before pelletizing.
If prepared EFB is stored in an open or humid environment, its moisture content may increase again.
To reduce this risk:
- Minimize storage time after drying.
- Use covered storage.
- Protect material from rain.
- Control warehouse humidity where practical.
- Use closed conveyors where appropriate.
- Avoid unnecessary exposure to outdoor air.
- Monitor moisture before pelletizing.
The production line should ideally be designed so that dried EFB moves efficiently from the dryer to the grinding and pelletizing stages.
Moisture Control During Different Seasons
Weather conditions can affect EFB processing.
In tropical palm-producing regions, high humidity and rainfall can influence raw material moisture and storage conditions.
During wet seasons:
- Raw EFB may contain more moisture.
- Drying requirements may increase.
- Storage becomes more important.
- Moisture reabsorption may become more significant.
During drier periods, the initial moisture may be lower, reducing the drying load.
Therefore, the operating parameters of an EFB pelletizing line may need to be adjusted according to seasonal conditions.
Moisture and EFB Pellet Machine Capacity
Moisture can influence the actual output of an EFB pellet mill.
A machine’s nominal capacity does not guarantee the same output under all raw material conditions.
If EFB is too wet:
- Pelletizing resistance can change.
- Die blockage may occur.
- Feeding may become unstable.
- Production may decrease.
If EFB is too dry:
- Pellet quality may decline.
- Fines may increase.
- Operators may need to reduce production speed.
This means that capacity should be considered together with moisture and raw material characteristics.
When selecting an EFB pellets machine, buyers should provide the manufacturer with accurate information about initial moisture and desired final moisture conditions.
How Moisture Affects Energy Consumption
Energy consumption is a major consideration in biomass pellet production.
The dryer normally consumes significant thermal energy because water must be removed from EFB.
Every additional amount of moisture removed requires additional drying energy.
This means that over-wet raw material can increase production costs.
At the same time, excessive drying can also waste energy.
The objective should therefore be:
Dry Enough for Stable Pelletizing, But Avoid Unnecessary Over-Drying
This balance can help reduce energy consumption while maintaining pellet quality.
Electricity consumption is also influenced by grinding and pelletizing conditions.
If the material is difficult to process because of unsuitable moisture, the energy consumption of downstream equipment may increase.
Moisture and Pellet Cooling
Moisture management does not stop when the pellets leave the die.
Fresh EFB pellets are hot because of the mechanical energy and friction generated during compression.
A cooler removes heat and helps stabilize the pellets.
(Learn more: https://richipelletizer.com/counterflow-pellet-cooler/)
During cooling, some residual moisture may also be released.
An efficient cooling system can therefore contribute to:
- Lower pellet temperature
- Better pellet hardness
- Improved storage stability
- Reduced condensation risk
- More stable final moisture
After cooling, the pellets should be screened and stored under suitable conditions.
Common EFB Moisture Problems and Solutions
Problem 1: Pellets Are Soft
Possible cause: Excessive moisture or insufficient compression.
Solution: Check raw material moisture, particle size, die condition, and compression ratio.
Problem 2: Excessive Fines
Possible cause: Material is too dry, particle size is unsuitable, or compression is insufficient.
Solution: Check moisture and pellet mill operating parameters.
Problem 3: Die Blockage
Possible cause: Excessively wet or sticky material.
Solution: Check dryer performance and feeding conditions.
Problem 4: Unstable Feeding
Possible cause: High moisture causing fibers to stick together.
Solution: Improve drying, storage, and hopper design.
Problem 5: High Energy Consumption
Possible cause: Excessive moisture or inefficient drying.
Solution: Monitor initial moisture, dryer efficiency, airflow, and final moisture.
Problem 6: Pellets Crack After Cooling
Possible cause: Improper moisture, insufficient bonding, or cooling conditions.
Solution: Check moisture before pelletizing and cooling parameters after production.
How to Optimize Moisture Before Pelletizing
A practical moisture management strategy can include several steps.
Step 1: Test Raw EFB
Measure the moisture content of incoming material.
Step 2: Remove Excess Foreign Material
Clean the EFB before size reduction and drying.
Step 3: Shred Long Fibers
Reduce the physical size of the EFB to improve drying efficiency.
Step 4: Dry the Material
Use an appropriately sized drying system.
Step 5: Measure Moisture Again
Check whether the material has reached the desired processing condition.
Step 6: Grind the Dried EFB
Create a suitable particle size distribution.
Step 7: Check Moisture Before Pelletizing
This final check can help prevent unsuitable material from entering the pellet mill.
Step 8: Monitor Pellet Quality
Observe pellet appearance, durability, fines, and production stability.
This process creates a feedback loop between raw material preparation and pellet mill operation.
Moisture Should Be Managed as Part of the Whole Production Line
One of the most important principles in EFB pellet production is that moisture cannot be considered separately from other process parameters.
A complete process may look like:
Raw EFB → Shredding → Drying → Grinding → Moisture Testing → Feeding → Pelletizing → Cooling → Screening → Storage
Each stage influences the next.
For example, better shredding can improve drying efficiency. Better drying can improve grinding performance. Better grinding can improve pellet mill feeding. Stable feeding can improve pellet quality.
This means that a complete EFB production line should be designed as an integrated system.
How RICHI Can Help With EFB Pelletizing
For an industrial EFB pelletizing project, equipment selection should begin with raw material analysis.
Important information includes:
- EFB source
- Initial moisture
- Daily raw material availability
- Required pellet capacity
- Desired pellet diameter
- Final application
- Available energy source
- Factory layout
- Automation requirements
Based on this information, a suitable production line can be configured.
The system may include EFB shredding, drying, crushing, grinding, feeding, pelletizing, cooling, screening, conveying, dust collection, and packaging equipment.
The objective is to make sure that the dryer, grinder, EFB pellets machine, cooler, and other equipment operate as a coordinated system.
(view website: RICHI Pelletizer )
Conclusion
Moisture has a major influence on EFB pelletizing results. It affects almost every stage of the process, from raw material preparation and grinding to feeding, compression, cooling, and storage.
If EFB contains too much moisture, pellet formation can become unstable, energy consumption can increase, feeding problems may occur, and die blockage can become more likely. If the material is excessively dry, pellet durability may decrease and fines may increase.
The key is to maintain a suitable moisture condition rather than simply trying to remove as much water as possible.
A successful EFB pelletizing process combines moisture control with appropriate shredding, grinding, feeding, die selection, roller adjustment, cooling, and screening. Moisture should also be monitored at different stages instead of being estimated only by visual inspection.
When selecting an EFB pellets machine, buyers should therefore consider the complete raw material preparation system rather than evaluating the pellet mill in isolation. The dryer, grinder, feeding system, pellet mill, cooler, and storage system all contribute to the final result.
With proper moisture management and a well-designed production line, EFB can be converted from a wet, bulky palm oil residue into a more consistent and manageable biomass pellet product suitable for storage, transportation, and energy utilization.


